- Home
- About us
- Products
- Butt Fusion Machine
- Electrofusion Machines
- Socket Fusion Tools
- Plastic Extrusion Machines
- Plumbing Tools
- PE Pipe Fittings
- Flange Facing Machine
- Fire Protection Pipe Hanger
- A Series Butt Fusion Machines
- B Series Butt Fusion Machines
- A Pro Series Butt Fusion Machines
- Plastic Pipe Cutter
- A Max Series butt fusion machine
- Fusion Tools & Accessories
- Hinged Pipe Cutters
- Fusion Data Loggers
- Faqs
- News
- Certificate
- Contact us
FX200 Butt Fusion in Action: What Can the Finished Bead Tell Us?
publisherRUBR
time2026/09/02
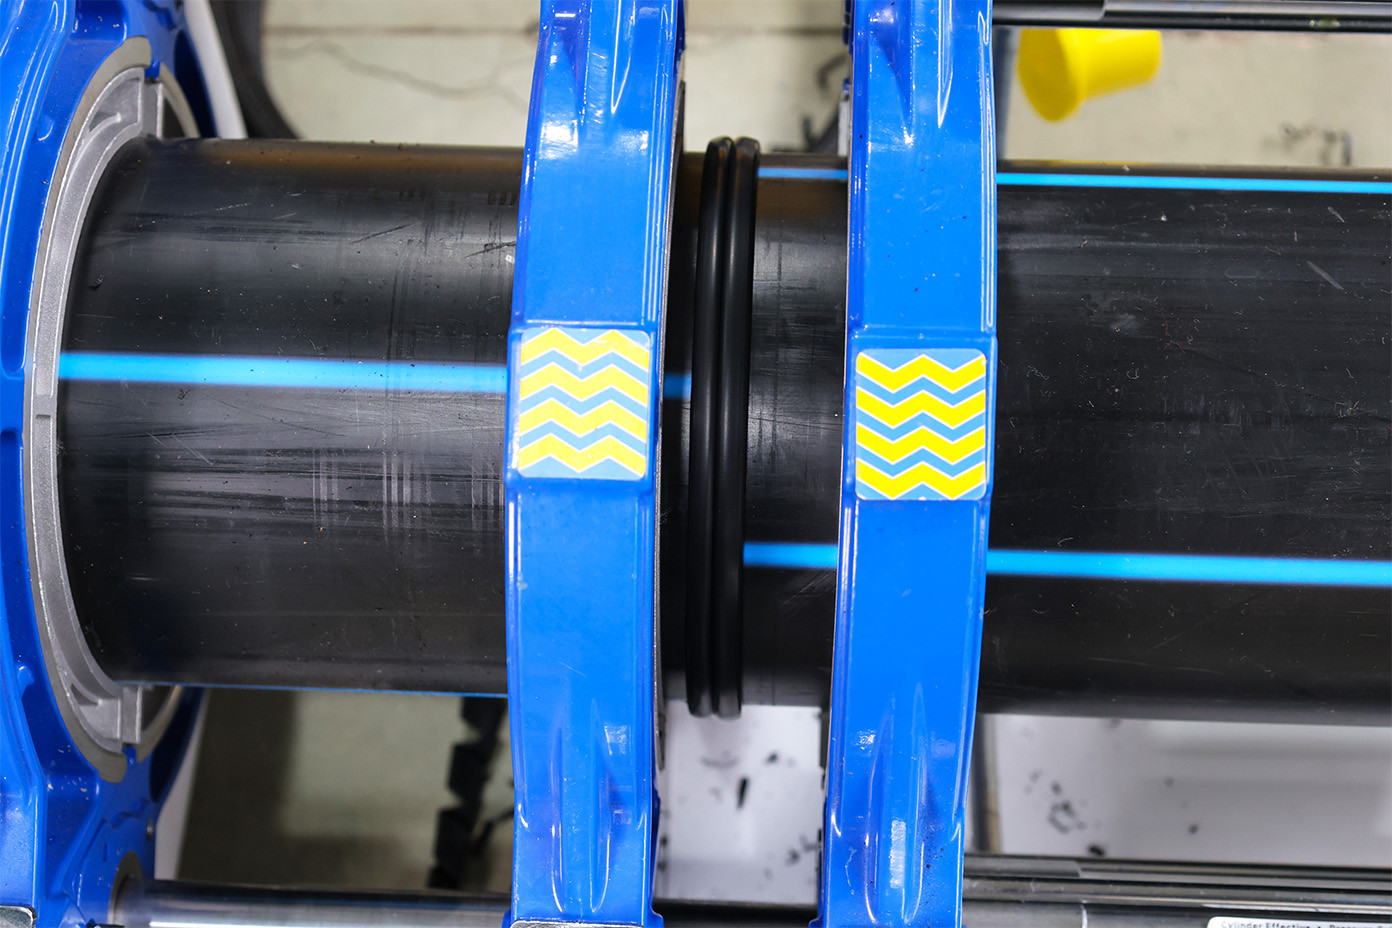
- A real-world look at the FX200 HDPE butt fusion machine, with a focus on the finished pipe joint and the key visual points to check on the fusion bead after welding.
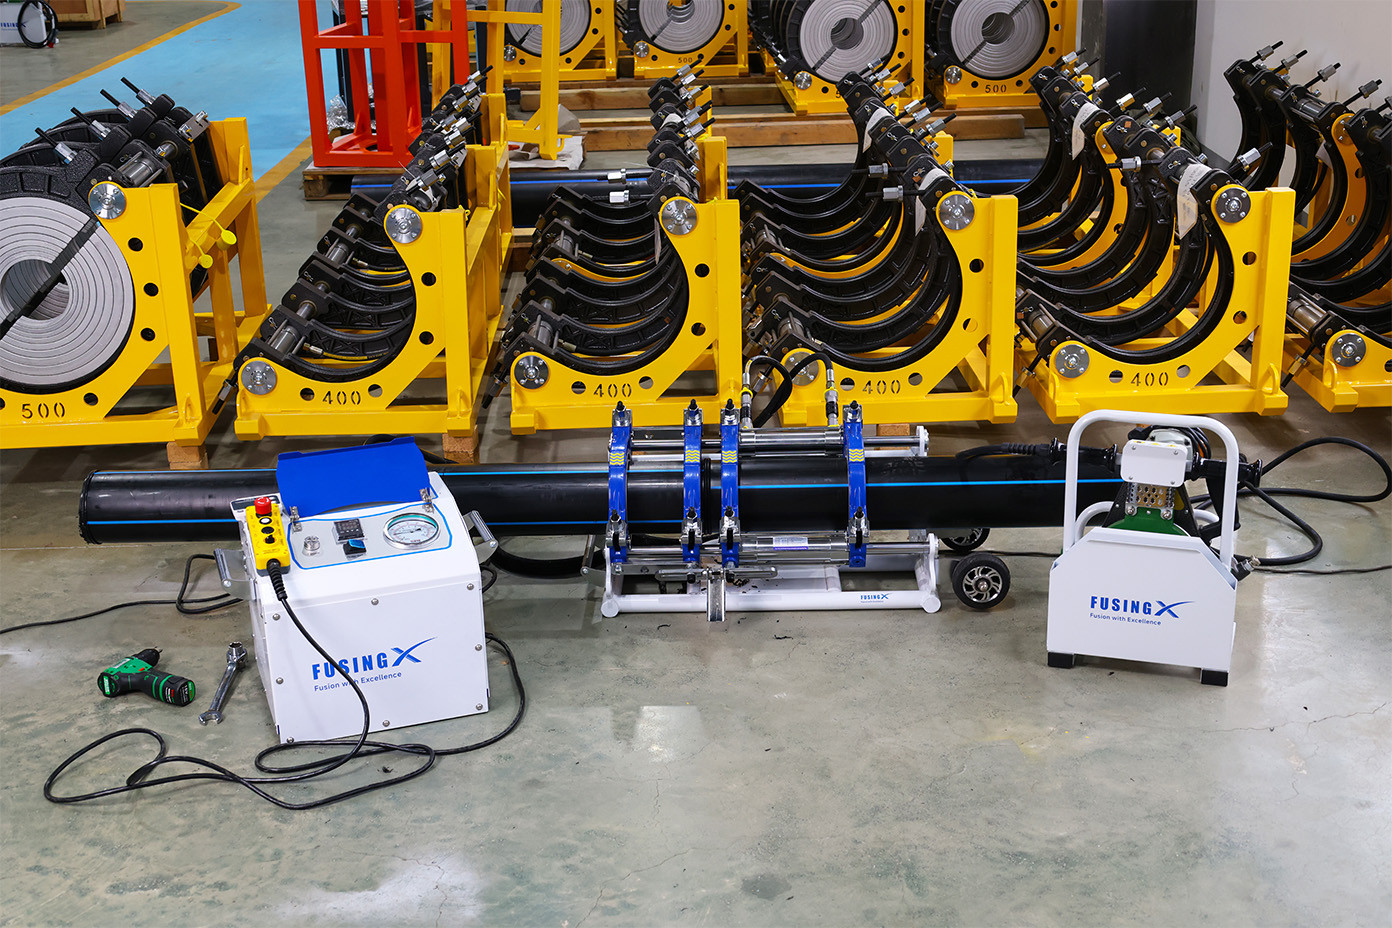
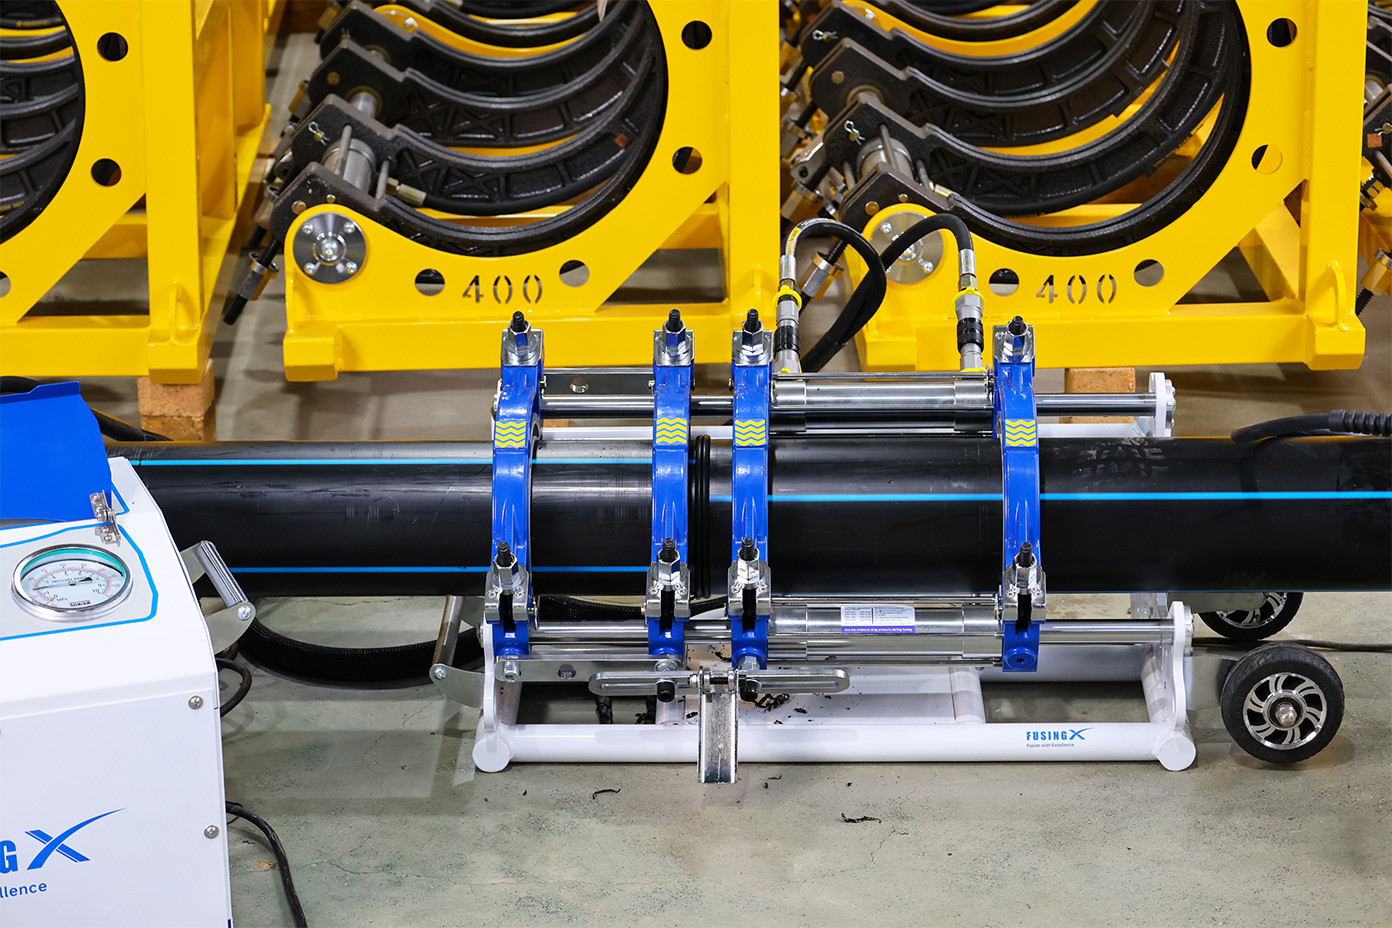
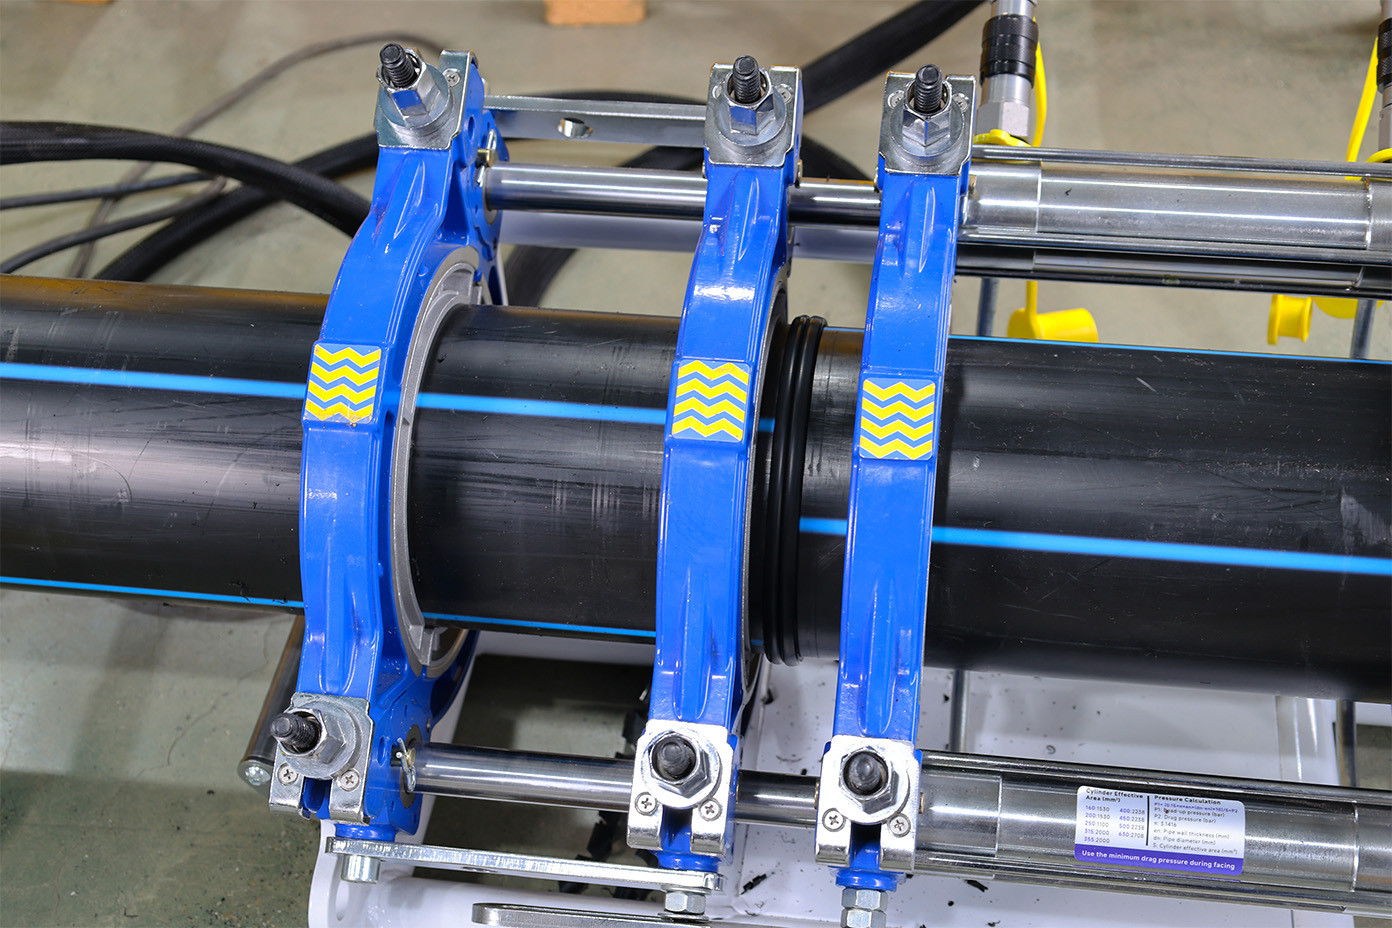
We recently captured a series of photos showing the FX200 before and after an HDPE pipe butt fusion job.
What makes these photos useful is not just the machine itself, but the finished joint. Once the fusion is complete, the bead becomes one of the first visible signs operators can check on site.
What to Look for After Fusion
A close-up of the finished joint can reveal several basic things at a glance.
Operators will normally look at whether:
· the bead is continuous around the joint;
· both sides are reasonably even;
· there are any obvious gaps or irregular sections;
· the two pipe ends show noticeable misalignment.
These visual checks do not confirm the full quality of a joint on their own, but they can help identify obvious problems before moving on.
A Bigger Bead Does Not Mean a Better Joint
This is an easy point to misunderstand.
The size and shape of a fusion bead can vary depending on pipe diameter, wall thickness, SDR, material, and the fusion procedure being used.
So a larger bead should not automatically be taken as a sign of better fusion.
What matters more is whether the bead is continuous and reasonably uniform, and whether there are any visible abnormalities around the joint.
It is also important to remember that bead appearance is only one part of the inspection process. Joint quality still depends on proper pipe preparation, heater temperature, heating time, changeover time, fusion pressure, and cooling time.
Where ISO, DVS, or another specified fusion procedure applies, those process parameters should still be followed accordingly.
From Machine Setup to the Finished Joint
The same photo set also shows the FX200 before fusion, giving a clearer view of the machine layout and working setup.
The FX200 is designed for PE pipe butt fusion from 63 to 200 mm, and these images provide a straightforward look at both the equipment and the final result it is intended to produce.
For butt fusion equipment, specifications tell you what the machine is designed to handle. The finished joint gives you a much more direct view of the actual work.